A 20 tonnes/day H-beam shop and a 200 tonnes/day shop should not buy the same line. Most suppliers blur that difference because their quotation template does. The honest split is simple: fit-up and handling decide whether automation pays, submerged arc welding is usually the first station that returns money, and straightening is the last.
At 20 tonnes/day, a full automated line often adds capital and maintenance without removing enough hours. At 200 tonnes/day, the same stations become bottlenecks that justify conveyors, automated fit-up, and tandem welding.
Fit-up: the station that decides the line
For a 400 mm flange, 8 mm web, and 12 m beam, manual fit-up with clamps and a tape takes 1015 minutes per beam when the parts are consistent. At 20 tonnes/day, roughly 1012 beams, that is 23 hours per shift. Automating fit-up does not save that whole block because the operator still checks flange square, web offset, and camber.
A hydraulic fit-up bed with fixed stops and a 1 mm feeler gauge is the right buy at this volume. A gantry with laser scanning and automatic clamping is not, unless you run the same section for weeks.
- At 20 tonnes/day: buy a fit-up bed, hydraulic clamps, and hard stops. Budget for one operator who understands mill tolerances, not a robot cell.
- At 200 tonnes/day: automated fit-up pays because 100130 beams per day turn a 15-minute manual task into a 20-hour labour problem.
- Watch the web thickness: below 6 mm, automated clamping can buckle the web; above 25 mm, clamp force and stop stiffness matter more than scan speed.
Tacking: usually not the automation you need
Tacking is where sales brochures get optimistic. A 46 mm tack every 300400 mm, placed by two welders, takes 35 minutes per beam on a well-fitted section. At 20 tonnes/day, robotic tacking rarely beats a semi-automatic gun and a good fitter. The tacks are also a distortion control tool: too large, and the SAW pass fights the tack; too small, and the joint opens during turning.
At 200 tonnes/day, automated tacking can hold cycle time, but only if fit-up is already within 1 mm and the line runs one family of sections.
Submerged arc welding: the real payback
SAW is the station where hours disappear. A 3.2 mm wire at 550 A and 30 V, traveling at 0.70.8 m/min, deposits roughly 45 kg/h in single wire. Twin wire pushes 810 kg/h. A 12 m beam with four 8 mm fillets carries about 48 m of weld; at 0.8 m/min that is 60 minutes of arc time, plus 1015 minutes for turning and interpass.
At 20 tonnes/day, one SAW gantry across two shifts can absorb that load if fit-up and handling are organised. At 200 tonnes/day, one gantry is not enough; you need tandem heads or multiple stations, and the layout must keep arc time above 50%.
Distortion control starts here, not at the straightener. Weld sequence from the neutral axis outward, backstep the first pass, and keep tack size at 5 mm rather than 8 mm. A 12 m beam that finishes with 3 mm/m sweep is a straightening problem; a beam that finishes with 1 mm/m sweep is a handling problem. The difference is usually sequence and heat input, not a bigger machine.
Straightening: dont automate at 20 tonnes/day
At 20 tonnes/day, a 200 t press and a flame straightening bench handle the occasional 5 mm camber over 12 m. The labour is 2030 minutes per beam, not every beam. A roller straightener at this volume sits idle and still needs setup for each section. At 200 tonnes/day, a roller straightener earns its place because 100 beams per day turn straightening into a full-time crew. Even then, keep a press for the 10% of beams outside the machines range.
Handling: the hidden hours
A 10 t overhead crane moving a 1.5 t beam takes 23 minutes per lift. Ten beams per day is 30 minutes; 100 beams per day is five hours of crane time before welding starts. At 20 tonnes/day, one crane and a turning gear are enough. At 200 tonnes/day, cross-transfer cars, roller beds, and magnetic turning stations remove the crane from the critical path. Do not buy conveyors for 20 tonnes/day unless the beam family is fixed and the floor space is already paid for.
The throughput figure you should not believe
Suppliers quote 812 minutes per beam, or 200 tonnes per shift, by assuming 100% arc-on time, no fit-up, no tacking, no turning, and no inspection. Real arc-on time in a mixed H-beam shop runs 4560%. Take a 12 m beam with 48 m of weld at 0.8 m/min: 60 minutes of arc, plus 15 minutes turning, plus 10 minutes fit-up check.
That is 8590 minutes per beam, not 10. At 20 tonnes/day and 1.5 t average, that is 10 beams and about 15 hours of station time. Believe the 50% arc-on figure, not the 8-minute claim.
| Station | 20 tonnes/day | 200 tonnes/day | Verdict |
|---|---|---|---|
| Fit-up | Hydraulic bed and stops | Automated fit-up gantry | Automate only above 100 tonnes/day |
| Tacking | Manual or semi-automatic | Automated tacking possible | Skip at 20 tonnes/day |
| SAW | One gantry, two shifts | Tandem or multiple stations | First station to justify |
| Straightening | Press and flame | Roller straightener | Do not automate at 20 tonnes/day |
| Handling | 10 t crane and turning gear | Conveyors and transfer cars | Automate only with fixed families |
Where the answer is dont buy
- Job shops running 20 tonnes/day with mixed sections: buy clamps, a fit-up bed, and one SAW column and boom. Skip robotic tacking, automated straightening, and conveyors.
- Shops without repeatable plate tolerance: fix the cutting first. A line cannot fit a 3 mm edge mismatch that the plasma table created.
- Shops below 50 tonnes/day with short runs: a second crane and a trained fitter will save more hours than a gantry.
If you are specifying a line, use the station-by-station numbers above and check the electrical and duty-cycle details against our welding equipment technical specifications before you sign.
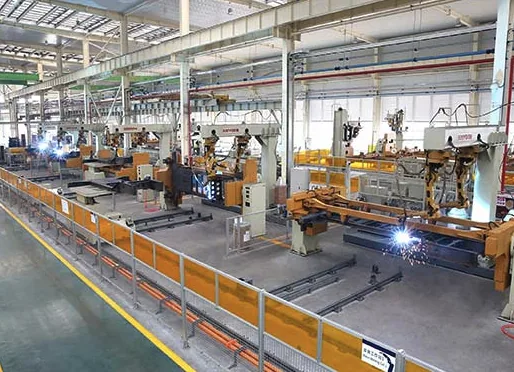
H-Beam Assembly Welding Line
Technical Specifications:
| Model | Web Height (mm) | Flange Width (mm) | Web Thickness (mm) | Flange Thickness (mm) | Length (m) |
|---|---|---|---|---|---|
| HBL-1000 | 200-1000 | 150-400 | 6-30 | 6-30 | 6-15 |
| HBL-1500 | 300-1500 | 200-500 | 6-40 | 6-40 | 6-18 |
| HBL-2000 | 400-2000 | 200-600 | 8-40 | 8-40 | 6-24 |
Note: Full production line: assembly tacking submerged arc welding straightening. CNC controlled. Production speed up to 20m/hour.
For detailed specifications and pricing, contact us at [email protected] or visit https://biqee.cn.
Conclusion
Choosing the right welding automation solution is key to improving productivity and quality in your fabrication operations.