The Number the Cell Has to Hold
Shops shopping for automation argue about robot reach, positioner payload, torch geometry and wire brand. The argument that actually decides payback is narrower: can the machine hold one number heat input, in kJ/mm inside its window, on every pass, for a full shift? Hold it and dilution, cracking, rework and cost per kilogram all fall in line. Lose it and no amount of payload saves the cell.
Heat input is arc power divided by travel speed: kJ/mm = (volts amps 60 arc efficiency) (1,000 travel speed in mm/min). Run 28 V and 300 A at 300 mm/min with an arc efficiency of 0.8 a reasonable figure for gas-shielded processes and you land at 1.34 kJ/mm.
Slow the same arc to 240 mm/min because someone on nights decided to “be safe,” and you are at 1.68 kJ/mm, a quarter of the way to the top of a hardfacing window before anyone has touched the voltage. Nothing on the machine changed except travel speed, which is the variable most often left to a teach pendant and an optimistic operator.
The window is tighter than it looks, and it is not one window for all work. High-chromium hardfacing on carbon steel runs roughly 1.2 to 1.8 kJ/mm. Structural carbon steel with SAW routinely sits at 2.0 to 3.0 kJ/mm and is happy there. Austenitic stainless is often capped lower, around 1.5 kJ/mm, to keep interpass temperature and sensitisation in check. A cell specified without a stated window per procedure is a cell that will drift to whatever feels smooth.
Dilution Is Decided Before the Arc Is Struck
Dilution the fraction of weld metal that came from the plate rather than the filler is not a settings-menu item. It falls out of heat input, travel speed and arc aim. On a chromium-carbide overlay, dilution above roughly 20% pulls iron into the deposit, drops hardness and converts a wear part into a maintenance schedule.
Below about 10% you buy the opposite problem: lack of fusion on the first pass and a hard, brittle layer that spalls under impact rather than wearing out. The 1.2 to 1.8 kJ/mm band for hardfacing exists to keep dilution inside those rails without losing fusion.
Arc efficiency belongs in the calculation, not in a footnote. Gas-shielded processes sit near 0.8; submerged arc runs nearer 0.95 because the flux blanket holds energy in the joint. A shop that carries a 0.8 factor into an SAW procedure is understating heat input by close to 20%, and will chase a cracking problem it created on paper.
What Running Cold and Running Hot Actually Cost
Below about 1.2 kJ/mm you get lack of fusion at sidewalls, poor tie-in on the first pass, and a fast-cooling deposit that shrinks hard against a cold substrate. Cracking that appears at the toe overnight is usually blamed on wire and is usually a preheat or heat-input problem.
Above about 1.8 kJ/mm on overlay work, dilution climbs, alloying elements are lost to the parent metal, the HAZ widens, distortion increases and the deposit softens a soft overlay wears quickly and quietly, so the failure shows up in service rather than at inspection. Both failures are expensive.
Only one of them gets caught in the shop.
Where the Money Goes on a Metre of Weld
Ask a fabrication shop what a metre of 25 mm butt weld costs and you will get a wire price. That is the smallest line in the model. On a 3 m Grade 350 single-V butt, filler metal runs about $24 roughly $8/m. Cell time, the preheat hold and the probability of a repair run three to five times that combined. Any argument about parameters has to be conducted in those terms, because that is where the money sits.
Five lines decide the price per metre. Arc-on time and deposition rate set everything downstream. Preheat and interpass hold is the line nobody quotes and everybody pays. Filler metal and flux is the visible line, and rarely the biggest. Rework the cold-crack tax is a probability weighted into every metre whether or not it happens on this one.
Distortion and fit-up is where automation both wins and loses: a cell holds a sequence perfectly, which reduces distortion, but it also faithfully welds a 4 mm gap that a human would have tacked shut.
A Three-Metre Butt, Priced Honestly
Submerged arc at 575 A, 31 V and 375 mm/min lays down roughly 13 kg/h and puts you at 2.7 kJ/mm. Drop travel speed to 300 mm/min “to be safe” and you buy 3.4 kJ/mm, more arc time than the joint needed, and a wider HAZ that pulls more distortion into the part.
On a 25 mm section the preheat soak is not a torch pass: at 80 C minimum for A36 in the 1030 mm range, the part needs to hold that temperature long enough for the section to equalise allow roughly an hour per 25 mm of thickness on a part with any mass, not ten minutes. A 2 m beam does not soak while the operator fetches coffee.
Add the rework line and the picture sharpens. If one joint in twelve needs excavation and re-weld, and a repair on this section costs 90 minutes of cell time plus consumables plus inspection, the repair contingency is a bigger line item than the $24 of wire. That is the correct frame for a capital decision: automation that halves repair rate pays for itself faster than automation that adds 2 kg/h of deposition, because the deposit only gets paid for once and the repair gets paid for twice.
Arc-On Time Beats Deposition Rate
Deposition rate sets the ceiling. Arc-on time sets the bill. A 5 kg/h process running at 30% arc-on deposits 1.5 kg per production hour; the same torch at 60% arc-on deposits 3.0 kg. Same wire, same power source, half the hours per kilogram. At a fully burdened cell rate of $85/h, that is roughly $57/kg of deposit against $28/kg a 50% swing with no change to the welding physics at all.
This is why the first automation question should be about loading, fixturing, spool changes, interpass waiting and inspection pauses, not about amperage. In most fabrication cells the largest single bucket is arc-off time, and the largest components of arc-off time are fixture design and the decision to wait for interpass temperature with the arc off and the operator standing there.
A second station, a rotation table, or a hard interpass limit written into the program will move the cost per kilogram further than any torch upgrade. Measure arc-on weekly, not monthly; monthly figures average away the shift that ruined the month.
Thermal Control Is a Data Problem, Not a Screen
A shop running two automated cells one structural, one hardfacing slag mill rollers with Fe-Cr-C on carbon steel had preheat screens in both programs and nobody checking whether the number on the screen matched the temperature on the part. Four of nine rollers came back cracked, not at the weld toe but spalling across the clad face after roughly 400 hours in service, on parts that should have run three to four times that.
The rework quote, including stripping and re-cladding, landed at $21,400 for the batch. The honest answer to “what did we do wrong” was that nobody knew, because nobody had data.
That is the characteristic failure mode of automated thermal control. The machine repeats a bad preheat perfectly, shift after shift, and logs nothing that would reveal it. Manual welding gets caught by the operator noticing the part is cold. Automation does not notice.
Preheat: Fix Uniformity Before Setpoint
Setpoints are the easy part. A36 plate in the 1030 mm range wants 80 C minimum; A514 wants 120 C. The failures happen in distribution. A torch pass that brings the surface to colour is not a soak, and a single thermocouple on the corner of a 2 m beam tells you about the corner.
What the procedure needs is a defined preheat zone, measurement at a stated distance from the joint on both sides, a soak time tied to section thickness, and a record that shows the part held the number rather than touched it. Two contact readings 300 mm apart that differ by more than 30 C mean the part is not soaked, whatever the screen says.
Interpass: The Number That Actually Kills Parts
Interpass temperature is where hardfacing jobs quietly fail. High-chromium deposits held too hot lose hardness and can spall in service; stainless held above its limit loses corrosion resistance and cracks later. Measure before every pass at the same location, not once at the start of the joint.
If the cell has no programmed dwell and no sensor, the interpass limit is decorative. The practical fix is unglamorous: a hard limit in the program, a contact pyrometer reading logged per pass, and a rule that the arc does not restart until the reading clears.
Shops resist the dwell because it looks like lost arc-on time. It is cheaper than a $21,400 re-clad.
PWHT Records That Match the Part
Post-weld heat treatment records commonly look excellent while the part warps or the hardness comes back wrong. The usual causes are thermocouple placement that measures the furnace rather than the part, heating rates that ignore section change, and hold times quoted per inch of thickness but applied to the thickest section on a part that is mostly thin.
For carbon and low-alloy fabrication, a hold around 600620 C at roughly one hour per 25 mm of section, with controlled heating and cooling above 300 C, is the ordinary starting point but the record must show part temperature at the defined locations, and the hardness survey afterwards must agree with it. When the two disagree, believe the hardness.
Matching the Process to the Wear Invoice
Hardfacing is a wear-cost decision before it is a welding decision. In bulk and minerals handling, abrasive wear accounts for roughly 67% of component wear, and the economics change again when the part runs hot a loader bucket handling slag above 500 C is a different problem from a conveyor chute at ambient.
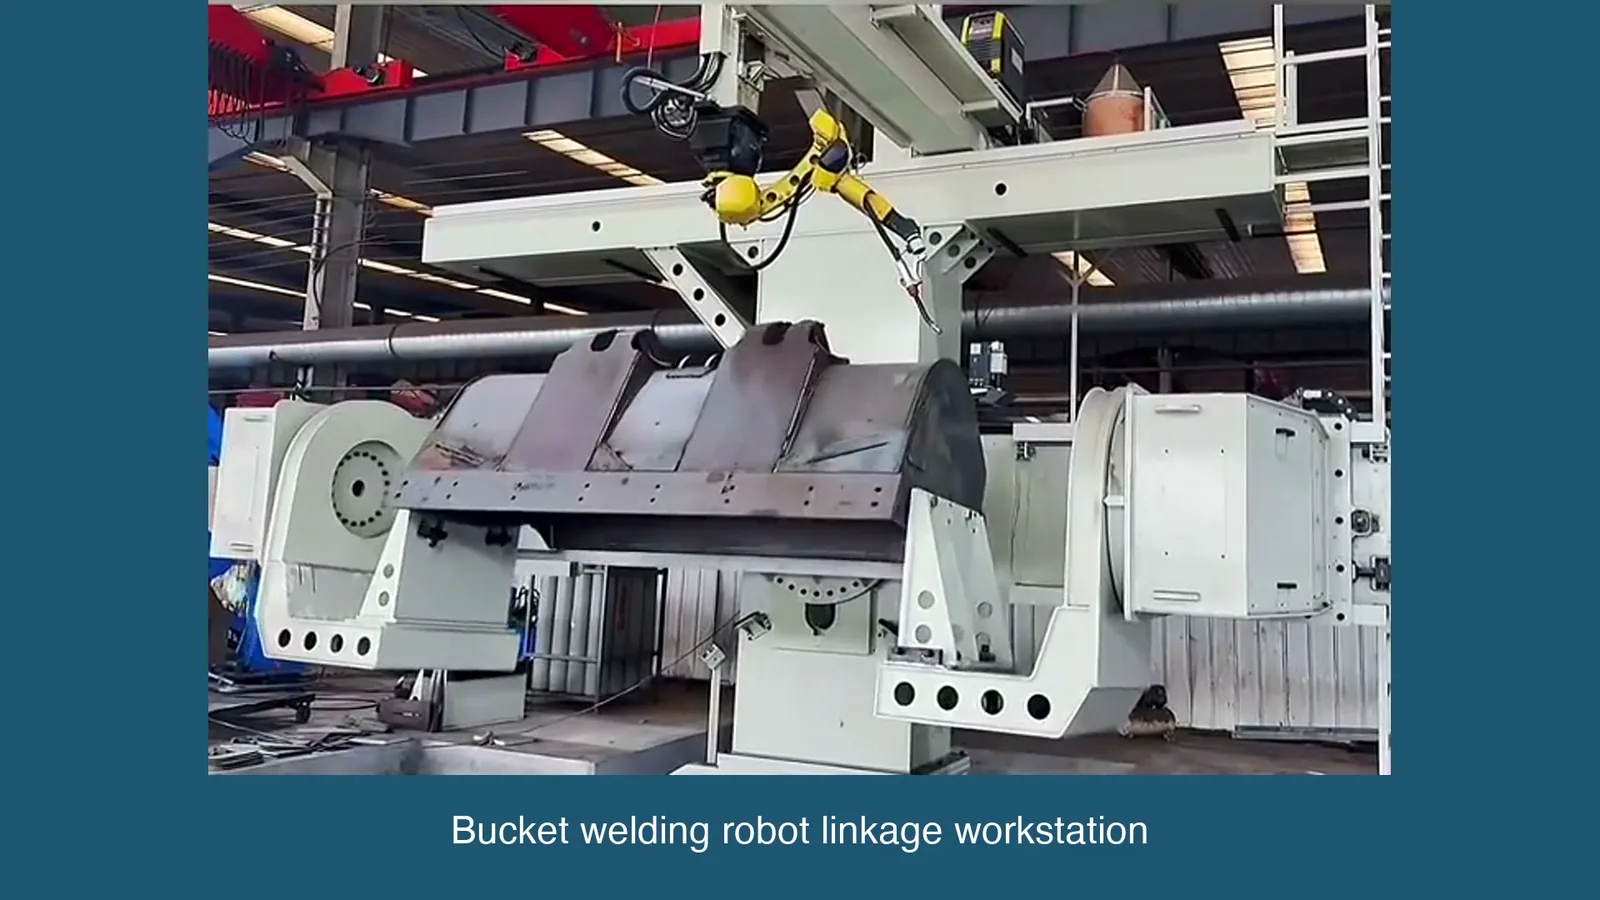
Automation can cut cost per kilogram of overlay, but only when the cell is selected against the wear mode, the overlay thickness and the real production volume. The useful question is not which machine, but which line of the cost model the process removes.
| Process | Typical deposition (kg/h) | Typical dilution (%) | Practical heat input (kJ/mm) | Single-pass thickness (mm) | Where it earns its place |
|---|---|---|---|---|---|
| Submerged arc, wire or strip | 814 | 1020 | 2.03.5 | 36 | Large flat or rotationally symmetric parts; high volume; thick overlay on mill rolls, tank shells, chute liners |
| Flux-cored, open arc | 36 | 1525 | 0.82.0 | 24 | Moderate volume, mixed geometry, buckets and lips; tolerant of fit-up, easy to deploy on gantries |
| GMAW spray transfer | 35 | 1015 | 0.61.5 | 1.53 | General fabrication and light overlay; good positional control; clean process, less post-weld dressing |
| Plasma transferred arc | 48 | 510 | 0.51.5 | 13 | Wear parts where low dilution preserves alloy cost; valve seats, pump components, precision reclaim |
| Laser cladding | 0.52 | 35 | 0.20.6 | 0.31.5 | High-value small parts, low distortion, thin overlay on finished geometry; slow and capital-heavy |
Read the table by the dilution column first if the overlay alloy is expensive, and by the deposition column first if it is not. A process at 5% dilution puts 95 cents of every alloy dollar on the part; one at 25% puts 75 cents on the part and the rest into the substrate, where it does nothing except soften the layer.
On a chromium-carbide wire, that difference funds a lot of capital. The heat input column is the constraint on which of these you can actually run inside a qualified window: high-deposition SAW is the cheapest per kilogram and the least able to hold a tight window on thin or distortion-sensitive work.
Where the Cell Stops Paying
Automation is not worth it in more cases than the equipment market admits, and a fabrication manager who says so early saves the company a write-off.
- Low part count. Below roughly 20 to 30 identical pieces per setup, programming, fixturing and first-article verification dominate. The cell spends its life being taught, not welding.
- Arc-on below about 2530%. At that point you have bought a fixture with a torch attached. Fix the handling problem with positioners and quick-change tooling before buying a robot.
- Fit-up variation beyond 2 mm on gap or mismatch. The cell will weld the gap it is given, defect and all, at full speed and with great repeatability.
- Thin, distortion-prone sheet where the acceptable heat-input band is below about 0.4 kJ/mm. Clamping, sequence and backstep rules start to cost more than the labour you removed.
- One-off repair and reclaim work with non-repeating geometry. Manual or semi-automatic hardfacing wins on anything that has to be measured before it can be programmed.
- Hardfacing below roughly 200 kg of overlay per month. The consumable saving from lower dilution does not recover the capital at that volume.
- Shops with no measurement culture. If nobody currently records preheat, interpass or arc-on time, a cell will industrialise the existing guesswork at higher capital cost.
There is a second honest boundary: automation does not fix a welding procedure that was never right. A cell holding a bad procedure will produce bad parts faster and with better documentation, which mostly means the failure is easier to trace and harder to argue with.
What Fails on the Floor, and What Stops It
- Hairline crack at the toe after overnight cooling, no alarm on the cell: check the preheat soak and the actual part temperature before touching the WPS. A cold part is the most common root cause, not contaminated wire.
- Hardface spalls across the face after a few hundred hours: suspect interpass running hot, then dilution. Pull the pass-by-pass temperature record before blaming the alloy.
- HAZ embrittlement or fatigue cracking at the toe: heat-input creep. Travel speed has drifted up or the program has been “optimised,” and the window is gone. Compare logged kJ/mm against the qualified value.
- Stainless cracking in service rather than in the shop: interpass and PWHT tolerance too wide. Tighten the interpass ceiling and confirm the hold temperature was measured on the part.
- Porosity that appears on one shift only: gas flow, torch angle or wire lot, in that order. Check the log for arc-on time and stops per hour frequent restarts at the same spot draw porosity.
- PWHT records good, part warped or hardness wrong: thermocouple placement and heating rate. Verify with a hardness survey and treat the survey as the record of truth.
What Goes Into the Specification
Most of what decides whether a cell pays back is settled in writing before the purchase order, and almost none of it is about the robot.
- A stated heat-input window per qualified procedure, in kJ/mm, with the arc efficiency value declared and justified for each process.
- Closed-loop control of current, voltage and travel speed, not preset values that drift with torch height and cable condition.
- Data logging at 1 Hz or better for voltage, current, wire feed speed, travel speed, arc-on and arc-off time, with an exportable file that survives the warranty period.
- Temperature measurement at defined locations in the preheat zone, with soak time recorded, plus an interpass reading logged per pass at a fixed location.
- Acceptance criteria based on first-pass yield and repair rate per metre, not machine uptime. Uptime is a vendor metric; repair rate is a shop metric.
- A commissioning trial on instrumented plate: run the qualified procedure, log every pass for two weeks, and compare the recorded heat input against the calculated value before signing off.
- Training for the people who will read the logs, not just the people who will jog the pendant. The failure in the roller case was not a machine fault; it was that nobody owned the numbers.
Get those seven items into the contract and the cell has a chance of holding the one number that matters. Leave them out and the shop will spend the first year discovering, at production speed, which of its procedures were never in control to begin with.
Automated welding in other sectors
If you work across more than one sector, these guides use the same engineering logic with the numbers that differ by industry.
Conclusion
Choosing the right welding automation solution is key to improving productivity and quality in your fabrication operations.
Technical Specifications (BIQEE Welding Positioner):
Rated load capacity: 100kg 50,000kg
Tilt angle: 0 120 (variable)
Rotation speed: 0.1 2.0 rpm
Control: PLC / CNC servo (dual-mode)
Applicable process: MIG/MAG, TIG, SAW, Flux-cored