One number frames the whole decision
A 4,267.2 mm outside-diameter monopile seam with a 100 mm HSLA wall does not care about your organisation chart. It cares whether the root lands inside tolerance. A 1 mm root mismatch on a joint of that size can raise local stress concentration by roughly 30 percent under cyclic offshore loading, and the joint has to carry that load for 20 to 30 years of fatigue cycles in a corrosive marine environment.
Every automation decision in wind fabrication sits downstream of that fact. The question is not whether a cell can lay a prettier bead. It is whether you can hold fit-up, heat input and travel speed tightly enough that the stress concentration never gets built into the structure in the first place.
That reframing moves the argument away from arc-on time, where automation looks like a straightforward win, and towards variance, where it looks far more conditional. A manual crew with a grinder can produce an acceptable joint. It produces it by absorbing variance into labour hours.
An automated route produces it by absorbing variance into fixtures, bevel quality, and a qualified parameter window. Both pass the same design codes. They do not carry the same cost structure, and they do not fail in the same way.
Where the money actually sits on a wind weld
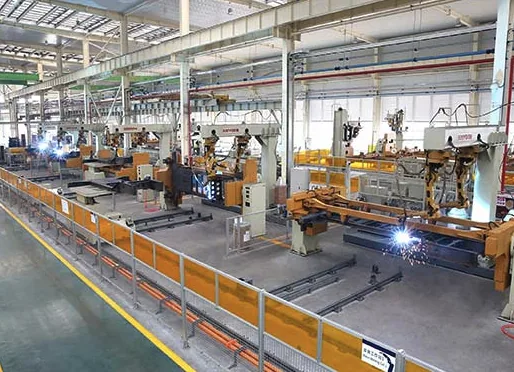
Read an automation proposal as dollars per metre of seam and dollars per kilogram of deposited metal, never as a machine price. For a typical automated GMAW cell running tower sections or monopile cans, the cost split looks roughly like this:
- 4555 percent cell time and labour, including operator, fixture handling and arc-on inefficiency
- 1015 percent fit-up and bevel preparation
- 812 percent consumables, shielding gas and power
- 1015 percent NDT and documentation
- 515 percent rework and heat-input correction
That last bucket is the one shops underestimate when they build the business case. Heat input is a parameter on paper and a rework line item on the floor. A cell running 15 percent above its qualified window because the travel-speed reference drifted does not produce obvious scrap it produces a seam that fails a hardness traverse or a toughness check three weeks later, after the section has been rolled out and the NDT crew has already signed the previous one.
Budget a cell hour rate of roughly 120 to 220 dollars or euros depending on region, and treat it as the denominator for every comparison. On a 3050 mm wall tower section, a machine-and-control route at 200 or more seams per year typically lands in the range of 95 to 120 dollars per metre of finished seam.
The grind-to-fit equivalent, once you load fit-up labour, rework and the occasional cut-out, commonly runs 140 to 180 dollars per metre at the same volume. At 40 seams a year those two numbers invert. The crossover is volume, not technology.
Two routes to the same round joint
Route A is the conventional shop floor. Plate is cut, edges are ground by hand, dimensions come off a tape measure, the joint is fitted and tacked, and welding is done semi-automatically with SAW or GMAW. It is flexible, it tolerates late engineering changes, and it works. Its defining characteristic is that variance is pushed into the joint rather than removed before the arc starts.
Route B moves end preparation and welding into a controlled sequence: CNC or orbital beveling, machine fit-up against a fixture or a set of hard stops, a defined root gap, and an automated weld with logged parameters. On an onshore tower section of 3,000 to 4,000 mm OD, Route A might see a 1.5 mm root gap and a 1.0 degree bevel variation running down the seam because that is what the grinder and the tape produced that shift.
Route B targets a 2 to 3 mm gap and holds bevel angle inside a fraction of a degree across the full circumference.
Both routes can satisfy EN 1090-2, DNV-ST-0126, AWS D1.1/D1.1M and ISO 15609. Compliance is not the differentiator. The differentiator is how many hours of a skilled grinder’s day disappear, and whether the resulting seam is repeatable enough to make NDT and rework predictable.
Fit-up is a stack-up, not a single dimension
Fabrication managers routinely treat root gap as the fit-up problem. It is one term in a stack that includes plate rolling ovality, cut-edge squareness, bevel angle, root face height, circumferential alignment, hi-lo at the seam, tack weld quality, and thermal movement between tack and weld. Automation closes the stack only if it closes every term in it. Buying a welding cell to fix a bevel problem is an expensive way to discover that your rolling mill is out of round.
The practical sequence is to measure the stack before specifying the cell. Record ovality on ten consecutive cans, record bevel angle on the same ten, record hi-lo at four quadrants. If ovality varies by more than 3 mm across the population, no fixture will save the root. If bevel angle varies by more than 1.5 degrees, a machine bevel is the first purchase, not a welding cell.
For fatigue-critical circumferential seams, target hi-lo under 1 mm and root gap at 2 to 3 mm with a documented tolerance band. That is achievable with machine fit-up and is not reliably achievable with tape and wedge. Where it is achievable by hand, the incidence of root repair drops enough that the automation case weakens considerably which is worth knowing before you sign.
Heat input: the WPS is the instruction set, not the paperwork
ISO 15609 requires the welding procedure specification to define heat input, and the procedure qualification record to validate it. In practice the PQR fixes the window and the WPS turns it into a number an operator can check. If the WPS says 1.2 kJ/mm, the shop needs a calibrated ammeter, a calibrated voltmeter, and a travel-speed reference good enough to prove it. A WPS with no calibration sticker behind it is theatre.
The arithmetic is simple enough to put on a whiteboard: heat input in kJ/mm equals voltage times amperage times 60, divided by 1000 times travel speed in mm per minute. Run 650 amps at 30 volts and 900 mm/min and you get 1.3 kJ/mm. That is a perfectly good number for a 40 mm S355 seam and it is outside a 1.2 kJ/mm window by eight percent, which is exactly the size of drift that goes unnoticed for six months and then shows up as a hardness excursion.
For 3080 mm S355 tower work, typical controls run a preheat of 100150 C and a maximum interpass of 250 C, with the interpass monitored at the seam rather than at the torch. The heat-input log is the cheapest quality tool in the cell: it catches the drift before the NDT crew does, and it is the evidence you hand a client when they ask how you know the seam was made inside the window.
Calibration is where the audit lands. Ammeters and voltmeters on a six-month interval, travel-speed verification on the machine before every production run, and a signature that ties the log to the operator and the seam ID. If the cell cannot produce that trail automatically, it is a semi-automatic machine with better marketing.
Matching the process to the seam
There is no single best automated process for a wind tower. There is a best process per seam family, and a shop that runs one process across all of them usually compromises on at least two.
| Route | Typical wall | Deposition rate | Heat input | Best seam | Where it fails |
|---|---|---|---|---|---|
| Single-wire GMAW, automated | 835 mm | 35 kg/h | 0.61.4 kJ/mm | Longitudinal seams on tower cans, root passes | Lack of sidewall fusion at high travel speed; poor tolerance to bevel variation |
| Tandem GMAW | 1550 mm | 812 kg/h | 1.02.0 kJ/mm | Long circumferential seams, high-volume tower work | Arc interaction sets narrow parameter window; needs tight gap control |
| SAW, single or twin wire | 2080 mm | 48 kg/h | 1.22.5 kJ/mm | Flat-position circumferential and longitudinal seams on cans | Requires rotation or positioning; flux handling adds rework risk |
| Narrow-gap SAW | 60120 mm | 610 kg/h | 0.81.6 kJ/mm | Monopile and transition-piece thick-wall seams | Wire positioning accuracy under 1 mm; poor fit-up is unforgiving |
| Orbital TIG | 312 mm | 0.31.0 kg/h | 0.30.8 kJ/mm | Nacelle hydraulic and fluid lines, 638 mm OD | Too slow for structural seams; sensitive to fit-up and purge quality |
| Hot-wire TIG cladding | Overlay, 34 mm per layer | 36 kg/h | Controlled dilution under 10% | Splash-zone corrosion-resistant overlay, wear faces | Cost per kilogram rises fast if dilution drifts above target |
The pattern is that deposition rate and tolerance to imperfect fit-up move in opposite directions. A tandem GMAW cell at 10 kg/h will not forgive a 4 mm gap. A single-wire cell at 4 kg/h will, at the cost of arc time. Specify the process after you have measured the fit-up capability, not before.
Defects that automation changes, and the ones it does not
Automation reliably reduces lack of fusion at the sidewall, because travel speed and torch angle stop being a function of operator fatigue at hour nine. It reliably reduces porosity caused by inconsistent gas coverage, provided the cell has a flow fault interlock. It reduces arc strikes and stray tacks because the arc starts where the program says it does.
What it does not fix:
- Root mismatch and hi-lo. These are set before the arc starts. Automation records them; it does not remove them.
- Dirty plate and moisture. Mill scale, oil and condensation cause porosity regardless of how the torch moves.
- Solidification cracking in thick sections. Governed by bead shape, manganese-sulphur ratio and restraint, not by machine repeatability.
- Angular distortion on longitudinal seams. Automation may reduce it through consistent heat input, but a badly sequenced weld will still bow a can.
- Plate rolling defects. An out-of-round can produces an out-of-round seam, faster and with better documentation than before.
That last point is the one that catches first-time buyers. Automation makes good processes faster and bad processes more visible. If the upstream problem is ovality or bevel quality, the cell will simply produce the same defect with a data log attached.
Cladding and hardfacing: buy by the kilogram
Corrosion-resistant overlay in the splash zone and hardfacing on wear-prone drive interfaces should be costed per kilogram of deposited metal, not per square metre of surface. Square-metre pricing hides dilution, and dilution is where the money goes. An overlay running 20 percent dilution needs roughly twice the layers of one running 9 percent to reach the same corrosion-resistant composition at the surface.
Target dilution under 10 percent with hot-wire TIG, 3 to 4 mm per layer, and two to three layers depending on specification. At 3 to 6 kg/h deposition and a deposit efficiency in the 6070 percent range for wire-based processes, the cost per kilogram of finished overlay is the number to compare between routes.
Hardfacing follows the same logic and pays back where the wear surface is a replaceable ring rather than a structural can if a wear face can be redesigned as a bolted insert, that is almost always cheaper than three decades of maintenance welding.
Sizing a line, and where automation stops paying
A mid-range tower line plate bending, longitudinal seam, circumferential seam and flange stations in one envelope typically runs 120 to 180 m of length and handles 4.3 to 5.0 m maximum section diameter with 35 to 55 mm maximum plate thickness. Throughput in that configuration is on the order of one tower section every three to five days, with the larger diameters and thicker walls at the slow end.
Those figures are useful as a sanity check: if your target output is one tower section per week, you are buying a line for a fraction of its capacity, and the per-seam amortisation never recovers.
Be explicit about where automation does not pay:
- Under roughly 1,500 m of annual seam length in a single geometry family. Fixture design, programming, procedure qualification and operator training do not amortise.
- One-off and prototype sections. A transition piece with unique geometry and a single unit to build is a manual job with a good WPS.
- Repair welding, field welds and root repairs. Too variable, too positional, and the volume is unpredictable by nature.
- Mixed-batch shops below roughly 200 tonnes per year. The cell sits idle between setups, and idle cell hours are charged at the full rate.
- Shops with a fit-up problem they have not solved. Automating welding upstream of an unresolved bevel or ovality issue converts a variable cost into a fixed one without improving the joint.
- Walls above 120 mm at low volume. Narrow-gap needs wire positioning accuracy under 1 mm and a qualification programme of its own; below a few hundred metres a year, contract the work out.
There is also a middle route that gets ignored: automate the bevel and the fit-up, keep the welding semi-automatic. On many 3,0004,000 mm OD sections, machine beveling plus a proper fit-up fixture removes most of the tolerance stack for a fraction of a full cell, and the residual welding variance is small enough that the 30 percent stress concentration penalty stops being a live risk. It is unglamorous and it is frequently the correct answer.
What to write into the specification
Specify the cell against the joint, not against the machine catalogue. The following clauses are the ones that decide whether the installation works eighteen months after commissioning.
- Fit-up capability, stated numerically. Root gap band, hi-lo limit, bevel angle tolerance and the fixture repeatability that delivers them, measured on production plate rather than test plate.
- Parameter control and logging. Current, voltage and travel speed logged per seam with a timestamp, seam ID and operator ID, exportable without a vendor licence. Retention matched to the 2030 year design life, not to a five-year IT policy.
- Calibration regime. Ammeter and voltmeter on a six-month interval, travel-speed verification before each production run, and a documented method for proving heat input without stopping the job.
- Procedure qualification plan. One PQR does not cover every joint in a tower. Plan qualification per joint type, per process, per thickness range and per position, following ISO 15614-1 ranges, and budget the destructive testing as part of the capital project.
- Operator competence. Manual welders are certified to ISO 9606 or the regional equivalent; automated cell operators need a separate competence record covering programming, parameter verification, fault response and the authority to stop the job. Write that into the training scope.
- NDT acceptance. Ultrasonic testing to ISO 11666 acceptance level 3 or the project-specified equivalent for structural seams, phased-array UT for walls above roughly 40 mm, magnetic particle or penetrant for surface-breaking indications, and radiographic or phased-array verification of the root on fatigue-critical circumferential seams. State the acceptance criteria in the purchase order, not in a referenced appendix nobody reads.
- Factory acceptance on production steel. A test seam on production plate, in the production fixture, cut and destructively tested before the final payment milestone. Not a demo on clean 20 mm plate.
- Pre-weld gate. The cheapest 30 minutes in the job is the check before the arc starts: bevel angle, gap, hi-lo, cleanliness, preheat measured at the seam, and consumable condition. Make it a signed step with a hold point, not a habit.
None of this is exotic. It is the difference between buying a welding machine and buying a manufacturing capability. The shops that get value from wind-sector automation are the ones that specified the tolerance stack first, the logging second and the torch last.
Automated welding in other sectors
If you work across more than one sector, these guides use the same engineering logic with the numbers that differ by industry.
Conclusion
Choosing the right welding automation solution is key to improving productivity and quality in your fabrication operations.
Technical Specifications (BIQEE Cutting & Bevelling):
Cutting thickness: 5mm 200mm (plasma up to 80mm)
Bevel angle: 0 60 (adjustable)
Cutting speed: 100 3,000 mm/min
Tolerance: 1mm per 10m of cut length